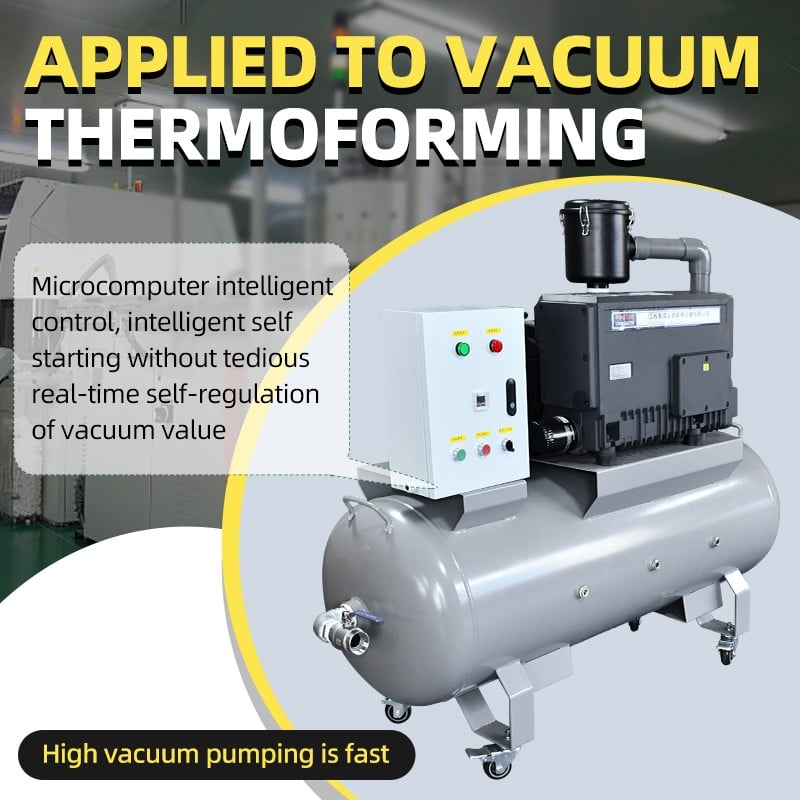
For a wide range of industrial processes including vacuum holding, resin degassing, vacuum drying and negative pressure conveying, a stable and controllable vacuum source is fundamental to consistent processing and finished product quality. As a well-proven and widely adopted vacuum generator, the oil-sealed rotary vane vacuum pump remains mainstream in the industrial vacuum sector thanks to its balanced performance. Jiangsu Youcheng Zhixin (YCZX) specializes in vacuum supporting solutions. With rich experience in equipment selection and export matching, we supply oil-sealed rotary vane pumps and complete vacuum system packages for global clients under diverse working conditions.
1. High Pumping Speed for Fast & Stable Vacuum Build-up
High pumping performance stands out as the core advantage of rotary vane pumps. Adopting mature vane technology, this series features a wide pumping speed range. It rapidly evacuates gas from closed chambers and builds stable industrial vacuum within a short time. Whether for batch intermittent operation or long-running continuous negative pressure on production lines, the pump maintains a smooth pumping curve. When paired with vacuum receivers to form a vacuum station, it effectively absorbs vacuum fluctuation and stabilizes line pressure. YCZX engineering team conducts precise selection based on chamber volume, required pull-down time and system leakage rate, to prevent over-sizing or insufficient pumping capacity.
2. Sufficient Ultimate Vacuum for Most Precision Processes
Ultimate vacuum defines the process limit of the equipment. The oil-sealed rotary vane pumps we supply can reach an ultimate vacuum of -0.1MPa (-100kPa), covering most precision industrial applications such as vacuum forming, degassing and vacuum clamping. Many buyers mistakenly pursue ultra-high vacuum blindly. We tailor solutions to match actual process requirements, balancing production cost and processing performance and avoiding unnecessary extra costs caused by over-specification.
3. Dual-function Oil Lubrication for Long-term Stable Operation
Long-term operational reliability is a top priority for industrial buyers. The oil lubrication system delivers both sealing and cooling functions. The oil film seals gaps between rotor, vanes and pump housing to block gas backflow and preserve vacuum level. Circulating oil continuously dissipates frictional heat and slows component wear for trouble-free long service. In YCZX export orders, many pumps are shipped as complete sets with vacuum receivers. All units pass strict factory inspection and export wooden case packaging to fit round-the-clock continuous operation at overseas plants.
4. Humanized Structure to Lower Workshop Operation Threshold
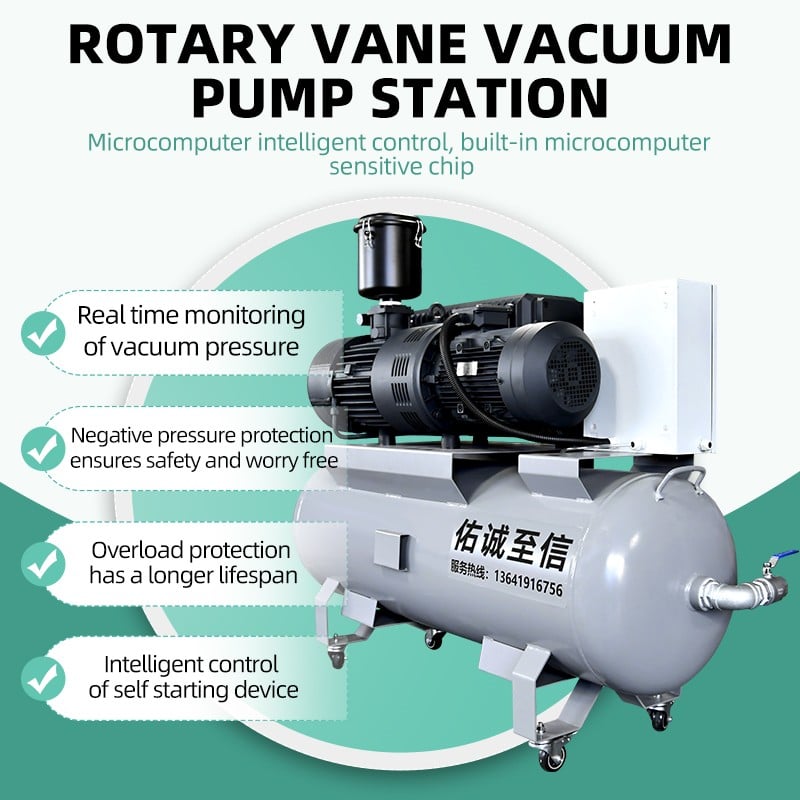
This pump is designed with practical on-site workshop requirements in mind. Optimized internal structure plus professional vibration damping reduces mechanical vibration and running noise, suitable for installation beside production lines or clean rooms where noise control is required. The standard air-cooled design eliminates extra water chiller and piping work. Flexible installation cuts initial capital investment and routine maintenance workload. Equipped with an integrated high-efficiency oil mist separator, it captures oil droplets from exhaust air for cleaner emissions and compliance with local environmental regulations.
5. Automatic Check Valve Protection to Secure Vacuum System
The built-in anti-backflow check valve acts as a critical safety barrier for the whole vacuum system. Once the pump stops, the integrated check valve instantly isolates the vacuum circuit. It prevents pump oil from flowing back into vacuum receivers and process chambers, avoiding oil contamination of workpieces and costly batch scrap. This safety feature is highly valued by customers with automated production lines. YCZX equips this protective structure as standard in our complete vacuum packages.
Overall, oil-sealed rotary vane vacuum pumps deliver a balanced combination of performance, safety and low maintenance cost, making them a highly versatile industrial vacuum solution. Following the design philosophy of all-round performance, intelligence and long service life, YCZX provides robust vacuum power support for industrial clients worldwide with professional selection service, standardized factory testing and reliable export support.

