For many industrial processes involving wet gas, steam, volatile media and oil-free vacuum requirements, the water ring vacuum pump station is a preferred vacuum solution. Unlike oil-sealed rotary vane pumps, liquid ring vacuum units excel at handling moisture-laden gas streams without oil contamination risks. Jiangsu Youcheng Zhixin (YCZX) designs, assembles and delivers complete water ring vacuum pump stations, covering technical selection, on-site matching, standardized packaging and global logistics support for industrial buyers worldwide.
1. Working Principle of Water Ring Vacuum Pump Station
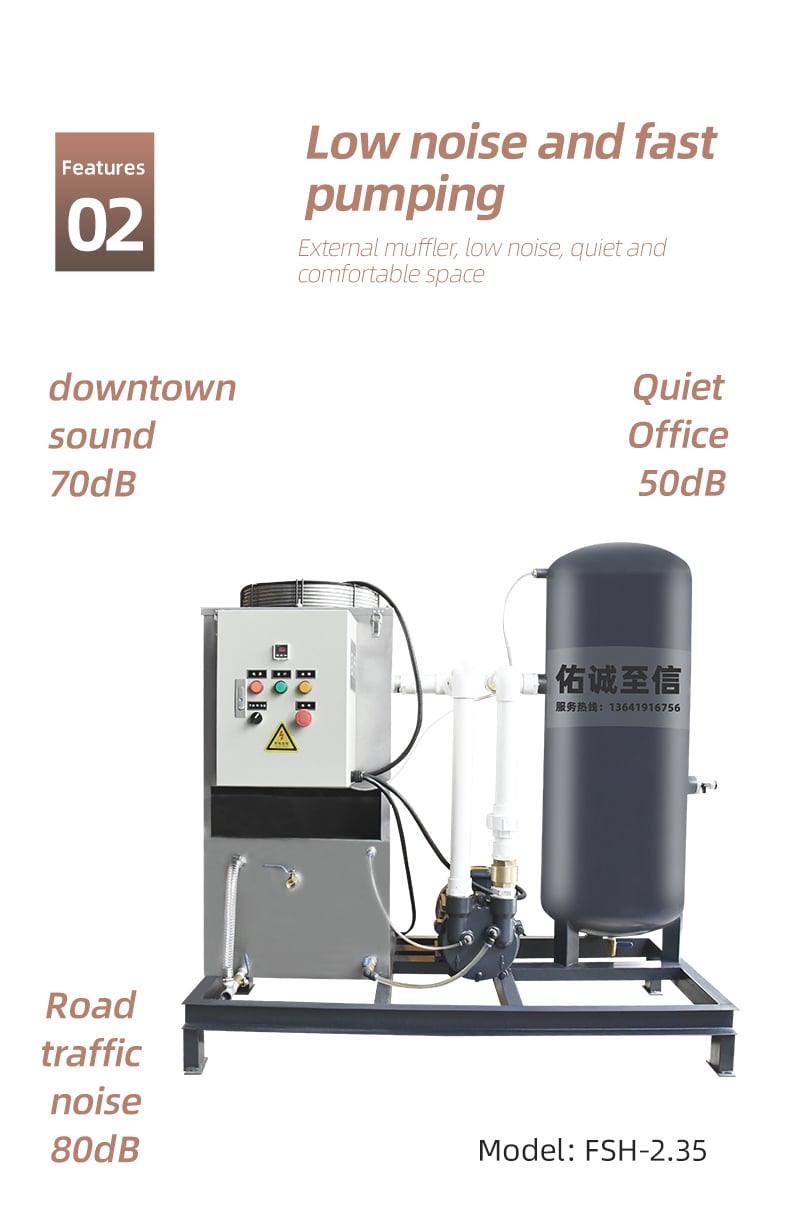
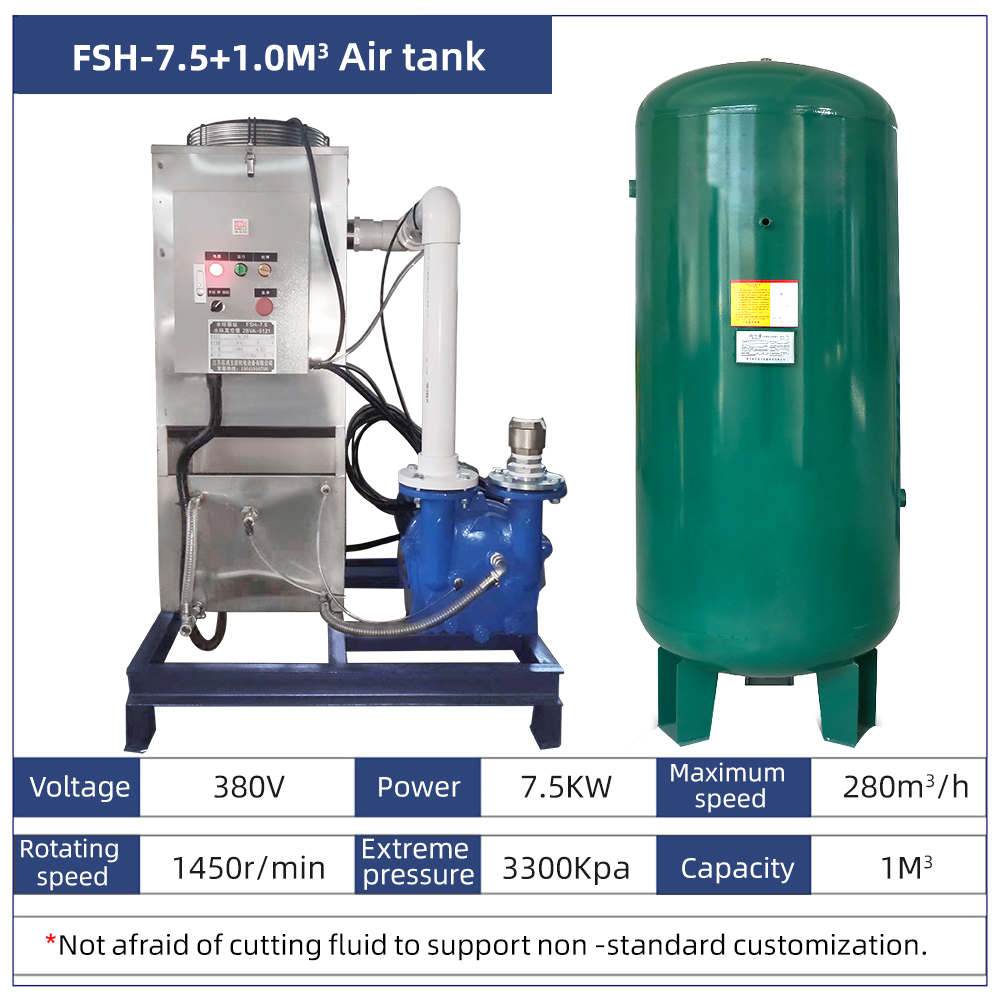
A water ring vacuum pump relies on liquid (usually service water) as the sealing medium. As the impeller rotates eccentrically inside the pump chamber, centrifugal force forms a rotating liquid ring. The changing volume between impeller blades and the liquid ring continuously completes gas suction, compression and exhaust. A full YCZX vacuum station integrates the water ring pump, vacuum receiver tank, control cabinet, pipeline, valves and water supply components into one compact skid-mounted unit, delivering stable negative pressure directly to production lines.
2. Core Functional Features
Oil-free Vacuum Output
There is no lubricating oil inside the pumping chamber, so no oil mist will mix into the extracted gas. This feature makes it ideal for processes where oil pollution is strictly forbidden.
Excellent Tolerance to Steam & Wet Air
It can reliably pump saturated steam, humid gas and a small amount of entrained liquid droplets, which is the biggest advantage over oil-sealed rotary vane vacuum pumps.
Stable Vacuum & Simple Maintenance
The structure is robust with fewer precision friction parts. Regular inspection of water quality, seal and liquid level is sufficient for long continuous operation.
Customized Protection Configuration
We can equip units with overload protection, water cut-off alarm, pressure interlock and explosion-proof motors for chemical and hazardous working conditions.
3. Typical Industrial Application Scenarios
YCZX water ring vacuum stations are widely deployed across multiple sectors:
- Chemical industry: evaporation, distillation, crystallization and solvent recovery
- Food & beverage: vacuum concentration, deaeration and vacuum impregnation
- Pharmaceutical: vacuum drying and material transfer
- Plastic & packaging: extrusion degassing and forming
4. Skid Packaging & Professional Global Shipment
Quality control does not end after factory testing. Every YCZX integrated water ring vacuum pump station goes through a full function test and pressure inspection before packing.For overseas shipments, we adopt customized export plywood crates or steel frame skid packaging. Key components such as the pump body, electric control box and gauges are wrapped with shockproof foam and fixed firmly to avoid displacement, collision and vibration damage during sea, air or land freight. Our team is familiar with international logistics requirements, container loading and marking standards. Whether delivered by FCL, LCL or air freight, we provide secure packaging solution and shipping documentation support.
Closing
Water ring vacuum pump stations are the go-to oil-free vacuum solution for wet gas processes. Balancing stable performance, low upkeep and flexible customization, they fill the gap where oil rotary vane pumps cannot work well. Supported by strict factory inspection, professional export packaging and reliable shipping arrangements, YCZX delivers complete vacuum systems with consistent quality to industrial partners all over the world.

